China Top Industrial Motherboard Suppliers for Global Buyers
China has become a major sourcing hub for Industrial Motherboard solutions used in factories, transport systems, medical equipment, and energy projects. Global buyers often seek stable performance, long service life, and flexible customization. The right supplier must provide more than a competitive quotation. Technical support matters.
Experienced manufacturers typically offer boards with extended temperature ranges, multiple expansion slots, and reliable interfaces such as COM, LAN, USB, and GPIO. These details become important inside dusty control cabinets or compact automation systems. A professional supplier should explain chipset selection, storage compatibility, BIOS options, and expected product availability. Clear documentation reduces integration delays.
Still, no supplier is perfect.
Buyers should review factory experience, quality procedures, sample results, and after-sales response before signing a contract. ISO certifications can support credibility, but certification alone does not prove every product will meet a project’s needs. Ask for thermal test data, vibration information, lifecycle planning, and traceable quality records. Site audits or video inspections may reveal practical details, including assembly discipline and testing equipment.
This guide examines leading China Industrial Motherboard suppliers from a global purchasing perspective. It considers product range, engineering capability, customization services, communication, and delivery reliability. The evaluation is not based only on polished websites or broad claims. Real performance depends on the application, environment, and supplier cooperation.
Some information may change.
Therefore, buyers should confirm current specifications and certifications directly with each manufacturer. A careful comparison can help companies reduce technical risk, control total ownership costs, and build longer-lasting industrial systems.
Industrial Motherboards: Form Factors, Functions, and 24/7 Applications
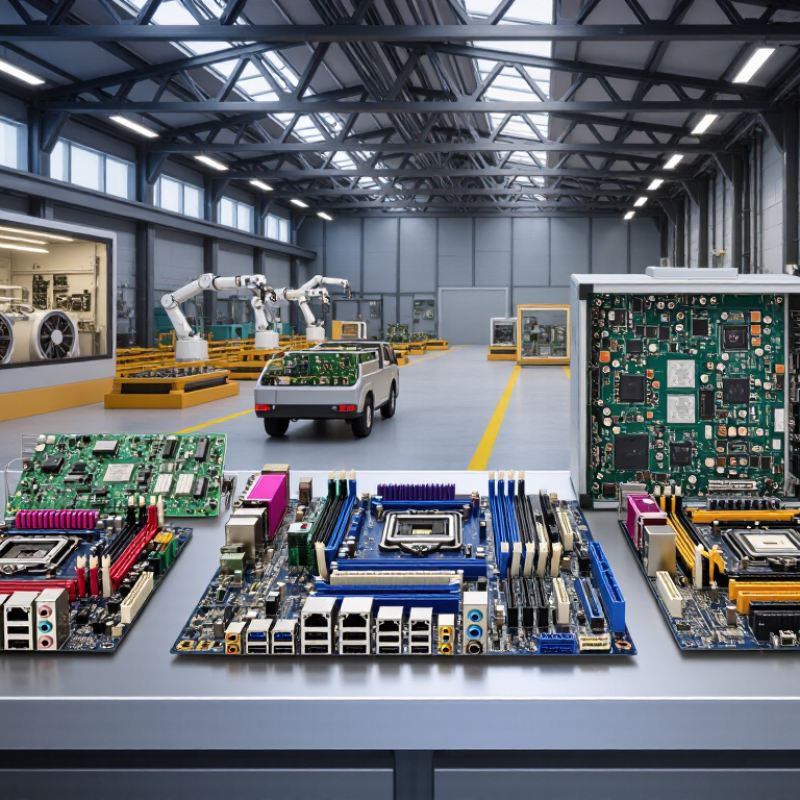
Industrial motherboards are built for machines that cannot afford casual downtime. ATX boards suit expansion-heavy systems, while MicroATX and Mini-ITX fit compact control cabinets. COM modules support modular designs, but carrier-board compatibility requires careful checking. A practical selection starts with I/O needs, not board size. Serial ports, GPIO, LAN, USB, display outputs, and storage interfaces should match the machine’s real workload.
Functions determine reliability during continuous operation. Look for watchdog timers, ECC memory support, TPM security, remote monitoring, and fan-control options. Wide-temperature components help equipment survive hot cabinets and cold production floors. According to IoT Analytics, connected IoT devices reached about 16.6 billion in 2023, with approximately 18.8 billion expected in 2024. More endpoints mean more gateways, inspection systems, and edge computers operating around the clock.
Thermal design remains easy to underestimate. A sealed cabinet may look clean, yet heat accumulates beside drives and power supplies. Industrial PC market research from MarketsandMarkets projects continued growth through 2028, driven partly by automation and edge computing. The numbers are encouraging, but forecasts are not guarantees. No motherboard is perfect. Engineers should test vibration, boot recovery, storage endurance, and long-duration thermal performance before deployment. Small details matter. A failed watchdog setting can stop an entire production cell.
Industrial Motherboard Form Factors for 24/7 Applications
Standard form factors differ significantly in board area, affecting expansion capacity, enclosure size, cooling design, and suitability for continuous-use systems such as industrial automation, edge computing, medical equipment, and transportation control.
China’s Top Supplier Types: OEM, ODM, and 5–15-Year Lifecycle Support
China’s industrial motherboard suppliers generally serve global buyers through OEM, ODM, or long-term lifecycle programs. OEM production follows an existing design, while ODM teams can adjust the board layout, I/O ports, BIOS, and thermal structure. This matters when a factory needs dual LAN ports, isolated serial interfaces, or a wide-temperature design. According to MarketsandMarkets’ 2024 Industrial PC Market report, the sector is projected to grow at roughly 6% annually through 2029. Buyers therefore need more than a low initial quotation.
An experienced supplier should define a 5–15-year support plan before mass production. The plan should cover component selection, approved substitutions, revision control, repair procedures, and final-order notices. WSTS reported that global semiconductor sales were forecast to rise 16% in 2024, reaching about 611 billion dollars. Such market movement can affect availability and pricing. A supplier with multi-source validation can reduce that exposure. Still, “lifetime support” is sometimes vague. Ask for written terms, annual availability targets, and a clear last-time-buy process.
For an OEM project, buyers should inspect production records, burn-in methods, and failure-analysis reports. For ODM work, review prototype evidence, thermal test data, and BIOS update controls. A five-year promise may fit office automation, but railway, medical, or factory systems can require fifteen years. That assumption needs testing. One overlooked connector can force a redesign. Pilot batches, sample audits, and quarterly engineering reviews make the partnership more reliable.